Megasonic Wafer Cleaning System Manufacturer: Key Factors for Semiconductor Fabs
2026-10-27
Choosing a megasonic wafer cleaning system manufacturer isn’t just a procurement checkbox—it’s a decision that directly affects particle removal efficiency, device yield, and long-term tool reliability in high-volume fabs. Yet with so many vendors making similar claims, how do you separate real process capability from marketing noise? This blog breaks down the key factors semiconductor fabs should weigh, from transducer design and frequency control to chemical compatibility and service responsiveness. As a specialist in advanced acoustic cleaning, Siansonic understands where subtle engineering differences become costly production problems. Whether you are qualifying a new supplier or benchmarking your current wet bench, the following criteria will help you make a choice that holds up under real fab conditions—not just in a datasheet.
Particle Removal Efficiency Beyond Marketing Data Sheets
Most datasheets for particle filters highlight a single efficiency number—typically at 0.3 µm, the most penetrating particle size, under a constant flow rate. That figure is handy for quick comparisons, but it says little about how the filter performs when the fan ramps up or down, when humidity spikes, or when dust begins to accumulate on the media. Real installations almost never match the test bench conditions.
A more meaningful metric is how well the filter holds its efficiency as loading increases. Some filters start at 99.97% and slide to 95% within a few weeks due to media compression, seal bypass, or uneven pleat spacing. Others maintain their rated removal far beyond the datasheet's nominal lifetime. To see the difference, you need to challenge the filter with a polydisperse aerosol and track downstream particle counts over days or weeks—not just at minute zero after installation.
Fractional efficiency across the full particle size range also matters more than a single snapshot. A filter can excel at 0.3 µm yet let through a surprising number of particles at 0.1 µm or 1.0 µm if the media has weak points or if the pleat geometry creates channeling. Look for fractional efficiency curves tested under cyclic flow, not just steady state. That is where the gap between marketing claims and actual removal performance becomes obvious.
Acoustic Energy Uniformity Across the Wafer Surface
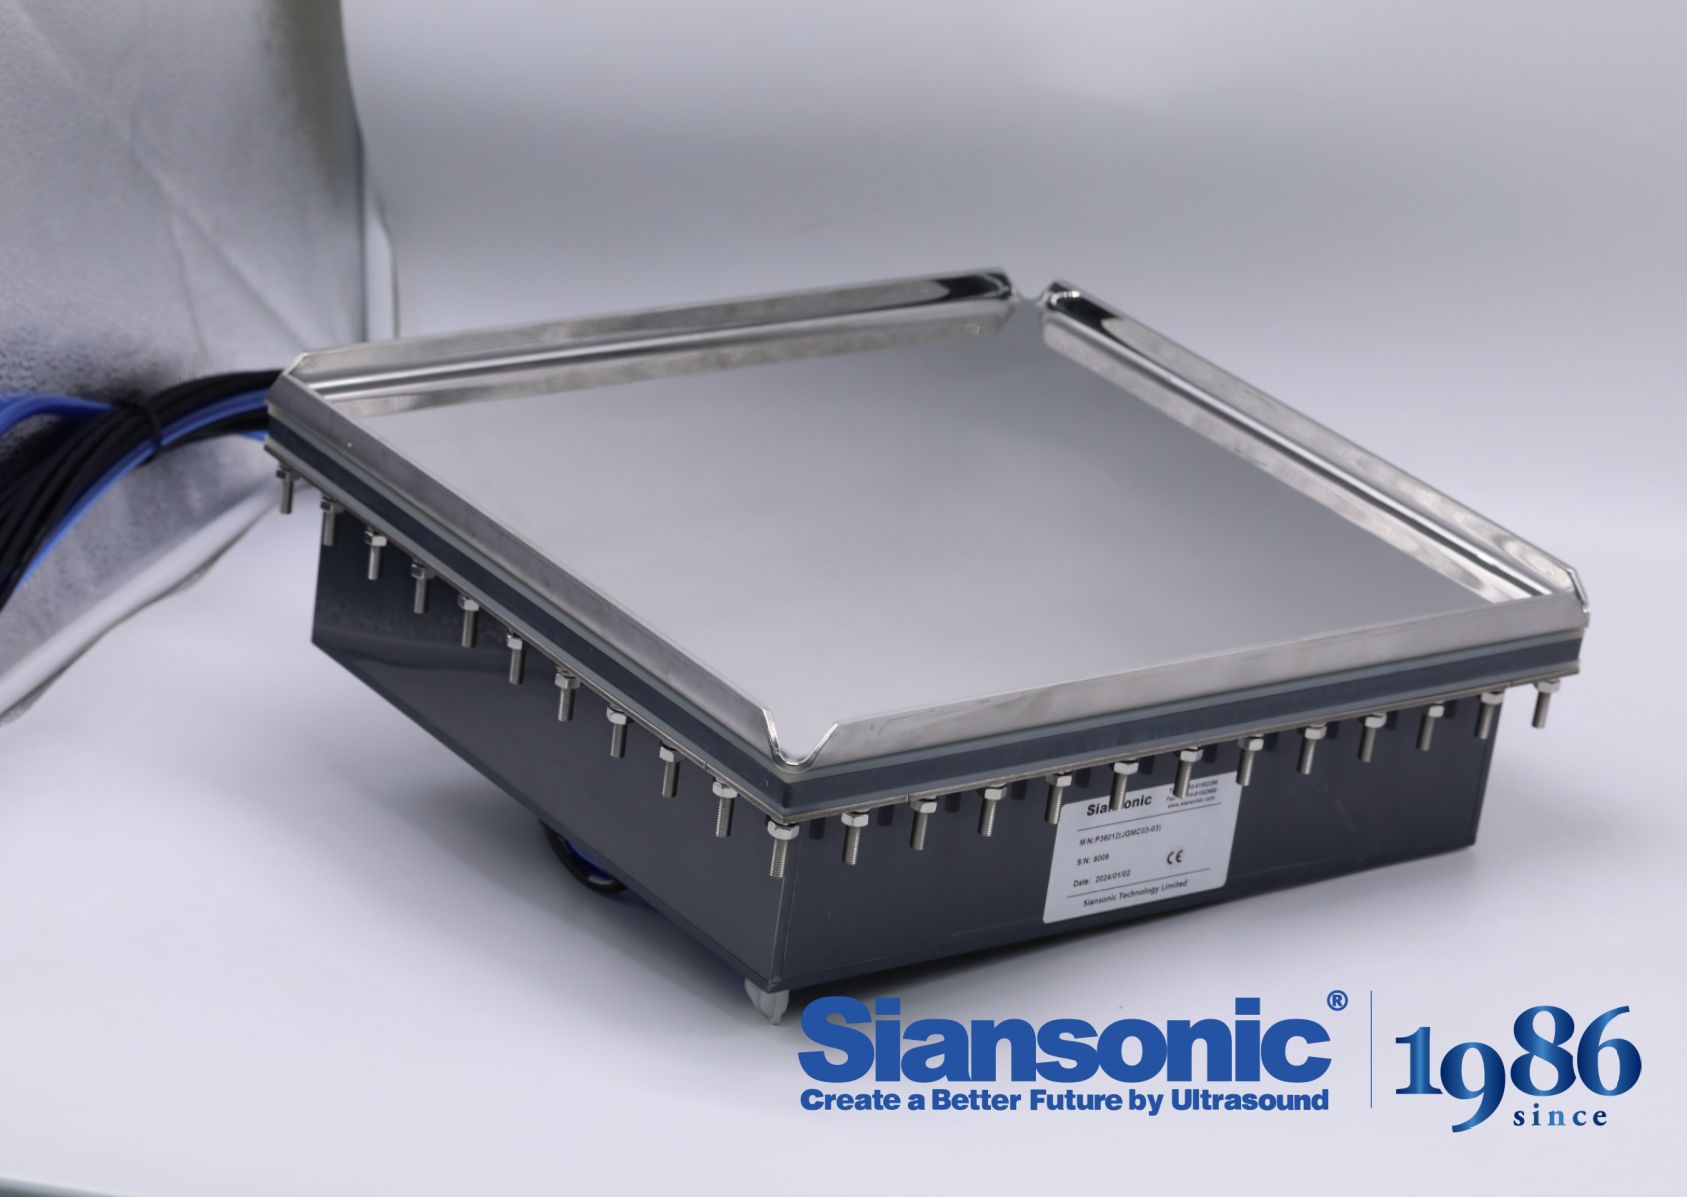
Variations in acoustic energy across a wafer are often revealed only after device yield drops. The edge, center, and intermediate zones do not receive identical exposure in most megasonic or ultrasonic cleaning baths, even when the transducer placement looks symmetrical. Standing waves, reflections from tank walls, and local attenuation through the liquid medium all create a spatial pattern that defies simple average power measurements.
Mapping this non-uniformity typically involves placing a hydrophone or a thin-film sensor at fixed radial positions, then comparing peak pressure or cavitation intensity. One practical approach is to rotate the wafer or alter the sweep frequency so that hot spots move across the surface. Without such compensation, repeated cleaning cycles can leave residue near the wafer edge while eroding delicate features closer to the center.
Achieving a tighter distribution means tuning both the transducer array and the fluid flow path. Some lines use multiple small transducers driven with slight phase offsets to smooth out nodes, while others adjust the gap between the wafer and the transducer face. The goal is not necessarily a perfectly flat map, but a repeatable envelope that keeps every die within the same process window.
Uptime Realities in High-Volume Manufacturing
In high-volume production, uptime is not a theoretical number but the actual rhythm of the plant floor. Even a chain of three-minute stoppages scattered across a shift can erase gains from incremental speed improvements. Managers often discover that a 95% uptime target still means seventy-two minutes of lost production every day—enough to miss shipment windows when buffers are thin.
The harder truth is that uptime losses rarely announce themselves. Wear on feeders, sensor drift, tool changes, and material jams accumulate quietly until a minor fault cascades into a blocked downstream station. Tracking only catastrophic failures misses the majority of lost time; small, frequent interruptions are the quiet drain on throughput.
Sustaining uptime demands more than scheduled maintenance. It requires line-level visibility into every short stop, operator ownership of first-line troubleshooting, and engineering that designs out fragile points. Plants that treat uptime as an operational habit rather than a maintenance metric see fewer fire drills and steadier output.
Chemical Consumption and Cross-Compatibility
Tracking chemical consumption across different stages of production often uncovers interactions that remain invisible on a standard material list. When two fluids share a delivery line, storage area, or even a common cleaning cycle, their compatibility determines whether residue accumulation, viscosity drift, or pH shifts will surface later. Rather than treating each chemical as an isolated input, operators pair consumption rates with a working compatibility chart to flag potential cross-contamination before it reaches a critical threshold.
A frequent oversight is assuming that low consumption equals low risk. In practice, trace amounts of an incompatible solvent or neutralizer can degrade the performance of a primary chemical over weeks or months. Cross-compatibility testing needs to cover not only the main ingredients but also reaction byproducts, temperature-dependent behavior, and interactions with seals, gaskets, and tubing materials. Field observations often show that sudden spikes in chemical waste correlate with unplanned mixing events, which turns consumption data into an early warning system for process integrity and material longevity.
Customizing Frequency for Thin and Bonded Wafers
Thin wafers, often ground below 100 microns, respond to acoustic or vibrational energy much differently than full-thickness substrates. Their reduced rigidity allows flexural modes to build quickly, which can cause edge cracking or localized delamination if the driving frequency remains fixed. Bonded wafer stacks add another layer of complexity: each material interface reflects or dampens energy depending on adhesive type, void distribution, and carrier thickness. A single standard frequency rarely balances both the need to reach buried bond lines and the need to avoid overstressing the thinnest regions.
Customizing frequency for these stacks usually means moving away from fixed presets. Some tools sweep through a narrow band around a center frequency, letting the system pass through resonant conditions only briefly instead of dwelling at damaging peaks. Others step between discrete modes selected from a measured impedance profile or a finite element model of the actual stack. For temporarily bonded wafers on glass or silicon carriers, shifting toward lower frequencies can spare the adhesive bond line, while short bursts at higher harmonics improve particle removal near the bevel. The most effective recipes treat frequency as a process variable tied to incoming wafer thickness and bond quality, not as a fixed machine constant.
Field Support and Process Engineering After Installation
Once a system goes live, the real test begins on the production floor. Our field support team embeds with your operators to catch subtle deviations—sensor drift, unexpected residue patterns, or shifts in ambient conditions—before they turn into downtime. Rather than waiting for a failure ticket, we schedule routine check-ins tied to your shift calendar, so adjustments happen during planned pauses instead of emergency stops.
Process engineering after installation moves beyond the original commissioning parameters. We pull trend data from the line and work back through the control loop to find opportunities the initial setup never anticipated—a faster ramp profile that still protects tooling, a purge sequence that cuts gas use by a third, a recalibrated setpoint that lets you run a new material grade without a full retool. These changes are tested in a sandbox mirror of your live configuration, then rolled out with a rollback plan already in place.
Documentation stays living, not shelved. Every visit ends with a brief, plain-language note in your maintenance log—what was checked, what was changed, and what to watch for next month. We train your in-house team on the revised procedures, ask them to run the next adjustment under observation, and leave behind a one-page cheat sheet tailored to the specific quirks of your line. Support is measured not by response time, but by how rarely you need to call.
FAQ
Look beyond basic specs. The real differentiators are how well the supplier handles uniformity across the entire wafer surface and whether their transducers maintain stable frequency under load. Also ask about their experience with your specific film stacks and device geometries.
Megasonic systems operate near 1 MHz or higher, producing gentler, more controlled cavitation than ultrasonic's lower-frequency bubbles. This reduces the risk of damage to delicate features while still removing sub-micron particles through acoustic streaming.
Even small frequency drift can create standing waves or dead zones on the wafer, leading to non-uniform particle removal. A reliable manufacturer designs transducers and drive electronics that lock onto the tank's resonance, compensating for changes in water level, temperature, and loading.
The system's wetted parts must withstand aggressive chemistries like SC1, SC2, or dilute HF without degrading or introducing contamination. High-purity quartz or PTFE components are common, but the manufacturer's cleaning and passivation procedures for metal parts matter just as much.
Run controlled tests with silicon nitride or polystyrene latex challenge wafers, then inspect using a surface scanner before and after cleaning. Look for consistent removal efficiency across the wafer, edge exclusion control, and repeatability over multiple cycles rather than a single impressive data point.
Transducer lifetime, ease of replacing quartz windows, and how quickly the tank can be drained and refilled all affect uptime. Ask manufacturers for realistic maintenance intervals and typical part replacement costs, not just MTBF claims.
Yes, many advanced fabs use megasonic nozzles or proximity heads for single-wafer cleaning. This approach allows better control of energy delivery and chemical exposure, but requires a manufacturer with expertise in nozzle design and acoustic field modeling for small gaps.
Look for SEMI S2/S8 compliance, CE marking where applicable, and documentation supporting cleanroom compatibility. Beyond certifications, ask for references from fabs running similar node sizes and wafer substrates.
Conclusion
When a fab evaluates megasonic cleaning suppliers, the first question is rarely about nominal frequency or tank size. It is about whether the transducer array actually delivers consistent acoustic pressure across the full wafer, not just at the center calibration point. A vendor can quote 99% particle removal on unpatterned silicon, but that number collapses on high-aspect-ratio structures if standing waves or dead zones exist. Fabs need to map energy density with hydrophone or erosion-test wafers across multiple recipes, especially for layers with metal or fragile low-k films. Uptime numbers from datasheets also deserve scrutiny: mean time between failures often assumes clean, low-temperature DI water and ignores real-world pump wear, cavitation damage to transducers, or sensor drift. In high-volume memory and foundry lines, a cleaning module that is down for two hours a week can silently become the bottleneck for the entire wet bench.
Chemical consumption is another hidden cost. A well-designed megasonic nozzle should reduce IPA or SC1 usage by improving mass transport, but many systems simply turn up power and flow rate to compensate for poor uniformity, which only adds waste and residue defects. Cross-compatibility matters when the same tool must handle silicon, SiC, GaN, or bonded stacks; an aggressive 1 MHz setting that cleans bulk silicon can crack a thinned 50 µm wafer or delaminate a hybrid bond interface. Suppliers who offer frequency sweeping or multi-zone transducers give process engineers room to tune for fragile substrates without sacrificing particle removal. After installation, field support makes the difference: a manufacturer that sends a real process engineer, not just a service technician, can help optimize recipes for new device nodes, adjust cavitation thresholds for novel films, and troubleshoot intermittent particle excursions before they become yield loss. These practical factors, rather than glossy spec sheets, define whether a megasonic cleaning platform survives a fab's qualification and remains productive at 90% utilization.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/